Top Heat Ceramic Coating Suppliers for Global Buyers
Global buyers need more than a long supplier list when evaluating Heat Ceramic Coating manufacturers. They need evidence of performance, process control, and dependable technical support. A coating may look flawless under showroom lighting, yet fail after repeated thermal cycling, vibration, moisture exposure, or poor surface preparation. That uncomfortable detail matters.
Professor Nicholas P. Padture, a leading thermal barrier coating researcher, described these materials as “an enabling technology for gas-turbine engines.” His statement reflects the industry’s central challenge: protecting metal components while supporting higher operating temperatures and longer service intervals. For buyers, this means examining more than coating thickness. Substrate compatibility, spray technology, porosity, bond strength, curing conditions, and inspection methods deserve equal attention.
The strongest suppliers usually provide technical data sheets, batch traceability, application guidance, and test results from realistic operating conditions. Ask how the supplier measures adhesion. Ask how defects are handled. Request samples when possible. A polished brochure is not proof.
Pricing also requires careful interpretation. A cheaper quotation can become expensive after premature repairs, rejected parts, or inconsistent batches. On the other hand, the most expensive option is not automatically the most reliable. Requirements differ across aerospace components, automotive exhaust systems, industrial furnaces, and energy equipment.
This guide compares leading Heat Ceramic Coating suppliers for global buyers. It considers product capability, manufacturing experience, quality systems, customization, delivery support, and communication. Some information may change over time. Buyers should verify current certifications and test documentation before making a final decision.
Ceramic Coating Types and Service Temperatures Above 1,000°C
Top Heat Ceramic Coating Suppliers for Global Buyers
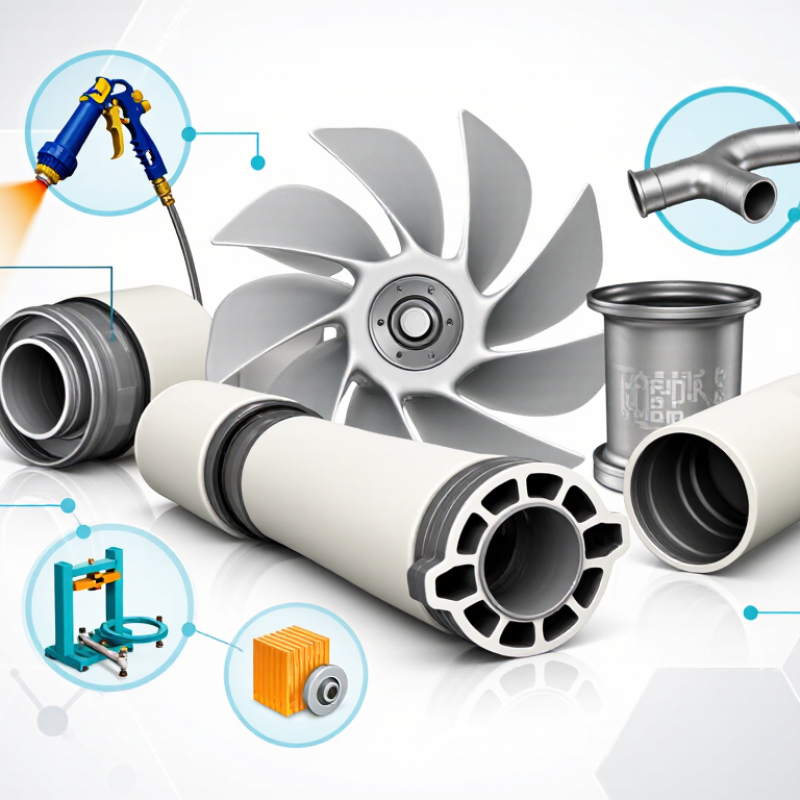
Ceramic coatings for temperatures above 1,000°C vary widely in chemistry and performance. Alumina coatings offer strong oxidation resistance and electrical insulation. Zirconia coatings reduce heat transfer, especially in thermal-barrier systems. Mullite and silica-based coatings suit furnace parts, kiln fixtures, and selected glass-processing components. Each type behaves differently during heating and cooling.
Service temperature must be checked as continuous, intermittent, or peak exposure. A coating rated at 1,200°C may fail under repeated thermal shock at 1,050°C. The substrate matters too. Steel, graphite, stainless alloys, and ceramic parts expand at different rates. Poor compatibility can cause cracking, flaking, or hidden delamination. Ask suppliers for test data, coating thickness, surface preparation details, and thermal-cycle results. A polished sample is not enough.
Practical evaluation should include furnace trials with real heating rates and atmosphere conditions. Observe the surface after several cycles, not only after one successful run. Some coatings need curing, controlled drying, or a roughened substrate. This step is often underestimated. I have found that supplier claims become less useful when test methods are missing. Request independent reports where possible, but inspect the assumptions behind them. A coating may survive 1,400°C in air yet perform poorly in vacuum, steam, or reducing atmospheres. That distinction can change the entire purchasing decision.
Key Performance Metrics: Emissivity, Thermal Conductivity, and Hardness
For global buyers, ceramic coating selection should begin with measured performance, not supplier promises. Emissivity shows how effectively a surface releases heat through radiation. High emissivity may reduce surface temperature in hot equipment, but test temperature matters. Ask for values within your operating range. A room-temperature result may mislead. Thermal conductivity describes heat movement through the coating itself. Lower conductivity can improve insulation, while higher conductivity may support heat spreading. The right value depends on the substrate, coating thickness, and heat-flow design.
Hardness indicates resistance to scratching, abrasion, and handling damage. It does not automatically prove thermal durability. A very hard layer can still crack during thermal cycling if adhesion or expansion matching is weak. Review pencil, wear, or indentation methods before comparing suppliers. Check coating thickness, curing conditions, surface preparation, and test standards. Small differences can change results significantly. Numbers need context. This is where many comparisons become imperfect.
Tips: Request independent test reports with the method, temperature, thickness, and substrate clearly stated. Compare emissivity and conductivity under similar conditions. Ask for thermal-cycle and adhesion data, not hardness alone. Inspect sample panels after repeated heating and cooling. Look for pinholes, discoloration, and edge lifting. Record the batch, cure time, and inspection date. A supplier willing to explain limitations may be more reliable than one offering perfect numbers.
Top Heat Ceramic Coating Suppliers for Global Buyers - Key Performance Metrics: Emissivity, Thermal Conductivity, and Hardness
| Coating Family |
Typical Supplier Offering |
Operating Temperature Range |
Total Hemispherical Emissivity |
Thermal Conductivity |
Microhardness |
Typical Applications |
Recommended Verification |
| Alumina (Al₂O₃) |
Dense or plasma-sprayed alumina ceramic coating |
600–1,200 °C |
0.80–0.95 |
1.5–3.5 W/m·K |
1,000–1,800 HV |
Electrical insulation, wear protection, furnace components, thermal barriers |
ASTM C1371, ASTM E1461, ASTM E384 |
| Partially Stabilized Zirconia |
Thermal-barrier coating based on zirconia stabilized with yttria or another oxide |
900–1,400 °C |
0.80–0.95 |
0.8–2.5 W/m·K |
600–1,000 HV |
Gas-turbine parts, engine components, exhaust systems, combustion hardware |
ASTM C1111, ASTM E1461, ASTM E384 |
| Silicon Carbide (SiC) |
CVD, pack-cemented, or spray-applied silicon carbide ceramic coating |
800–1,600 °C |
0.75–0.95 |
10–30 W/m·K |
1,800–2,600 HV |
Abrasive wear protection, semiconductor equipment, heat exchangers, high-temperature fixtures |
ASTM C1371, ASTM E1461, ASTM E384 |
| Silicon Nitride (Si₃N₄) |
Dense silicon nitride coating for thermal-shock and wear resistance |
800–1,400 °C |
0.75–0.90 |
10–30 W/m·K |
1,200–1,800 HV |
Molten-metal handling, semiconductor parts, furnace components, high-temperature bearings |
ASTM C1371, ASTM E1461, ASTM E384 |
| Hexagonal Boron Nitride (h-BN) |
Non-wetting, electrically insulating boron nitride coating |
800–1,000 °C in air; higher in inert atmospheres |
0.80–0.95 |
2–10 W/m·K |
10–50 HV |
Release coating, molten-metal processing, crucibles, electrical insulation |
ASTM C1371, ASTM E1461, ASTM E384 |
| Mullite (3Al₂O₃·2SiO₂) |
Mullite-based refractory or thermal-insulation coating |
1,000–1,500 °C |
0.80–0.95 |
1.5–3.0 W/m·K |
700–1,200 HV |
Kiln furniture, furnace linings, refractory components, thermal-processing equipment |
ASTM C1371, ASTM E1461, ASTM E384 |
| Alumina–Titania |
Thermal-sprayed alumina–titania wear and insulation coating |
500–900 °C |
0.75–0.92 |
1.5–3.0 W/m·K |
700–1,300 HV |
Pump components, textile machinery, electrical insulation, sliding-wear surfaces |
ASTM C1371, ASTM E1461, ASTM E384 |
Data note: The values shown are representative engineering ranges for ceramic coating systems and are not company- or brand-specific. Actual performance depends on coating thickness, porosity, substrate, deposition process, surface finish, measurement temperature, and test direction. Emissivity should be compared at the same wavelength and temperature, while thermal conductivity should be verified at the intended operating temperature.
Global Supplier Comparison by Capacity, Certifications, and Lead Times
Top Heat Ceramic Coating Suppliers for Global Buyers
Global supplier comparison should begin with usable capacity, not impressive factory size.
Ask for monthly output, standard batch volume, and available coating lines. Capacity is not everything. A supplier producing 20,000 units monthly may still struggle with urgent custom orders. Request recent production records, equipment lists, and sample panels from similar substrates.
Certifications require careful checking.
ISO 9001 supports process control, while ISO 14001 reflects environmental management. Automotive or aerospace applications may require additional sector-specific approvals. Verify certificate numbers, issuing bodies, expiration dates, and covered production sites. A certificate without matching scope offers limited assurance. Technical files should also include coating thickness, adhesion results, thermal-cycle data, and safety documentation.
Lead times often reveal a supplier’s real reliability.
Sample development may take 7–14 days, while repeat production can require three to six weeks. Confirm whether testing, packaging, customs documents, and inspection are included. Dates need evidence. Ask for a written schedule with milestone dates and escalation contacts. I have seen comparisons fail because buyers measured only factory speed, ignoring raw-material availability and export preparation. That weakness deserves attention. A smaller supplier with transparent planning may outperform a larger one during peak demand. Still, forecasts should remain conservative, because ceramic formulations and curing conditions can change after scale-up.