In 2026, global buyers will face a wider selection of Spray Welding Powder than simple alloy labels suggest. Nickel-based, cobalt-based, iron-based, and carbide-containing powders serve different repair and protection needs. Their performance depends on chemistry, particle size, hardness, substrate compatibility, and application temperature. A powder that performs well on a steel shaft may fail on a high-speed valve seat.
Industry data supports continued interest in surface engineering. Grand View Research and MarketsandMarkets have both reported sustained growth in the global thermal spray coatings market, driven by aerospace, energy, mining, automotive, and industrial equipment demand. These reports focus mainly on thermal spray technologies, not every spray welding process. That distinction matters. Buyers should avoid treating broad market forecasts as direct proof of one powder’s suitability.
Technical guidance from ASM International’s ASM Handbook, Volume 5A: Surface Engineering, emphasizes coating design, heat control, dilution, bond strength, and post-machining requirements. ISO 14923 also provides useful methods for evaluating thermal-sprayed coatings, although it does not replace process-specific validation for spray welding. Powder morphology matters too. Spherical particles may feed smoothly, while irregular particles can influence deposition behavior and packing density.
No single powder wins everywhere.
A practical 2026 comparison should connect alloy type with service conditions, including abrasion, corrosion, impact, temperature, and machinability. Buyers should request certificates, batch traceability, safety data sheets, particle-size distribution, and application references. Small details matter, such as a powder’s storage humidity or actual torch settings. Supplier claims still require testing. This is where many purchasing decisions become less certain, and more honest technical review is needed.
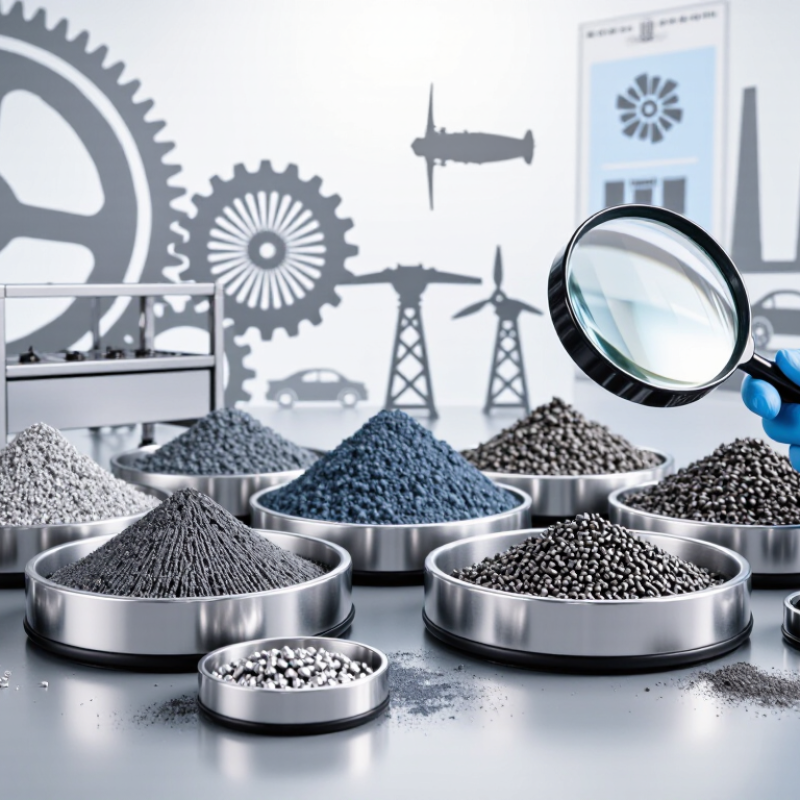
Spray welding powders are selected by particle size, alloy chemistry, and service conditions. For global buyers, 45–106 μm is a practical range for stable feeding and controlled deposition. The powder should flow evenly through the equipment. A narrow size distribution usually improves coating consistency. Too many fines can create dust and feeding problems. Excessively coarse particles may melt unevenly.
Nickel-based self-fluxing powders are widely used for wear-resistant repairs and protective layers. They can provide strong bonding after proper heating and surface preparation. Cobalt- and iron-based powders may suit higher wear, impact, or temperature demands. The correct choice depends on the base metal and operating environment. Hardness targets commonly range from 30 to 60 HRC. However, 60 HRC is not automatically better. A harder layer can become less tolerant of impact.
That assumption is convenient, but incomplete. In practical trials, clean, degreased steel often matters as much as powder selection. Technicians should control preheating, spraying distance, travel speed, and remelting temperature. These variables influence dilution, porosity, and final hardness. I have seen a powder meet its laboratory specification but perform poorly after rushed preparation. The defect was not always in the powder. Buyers should request particle-size data, hardness test conditions, chemical composition, and batch inspection records. Small details matter. Testing on a representative component remains the safest decision before large-volume purchasing.
Nickel-based spray powders remain practical choices when surfaces face abrasion, heat, and corrosive chemicals. Typical deposits reach 35–60 HRC, depending on alloy chemistry, particle size, and spraying method. HVOF usually produces dense coatings with low porosity, while fusing processes can improve metallurgical bonding. Hardness alone misleads. A 55 HRC layer may still fail if it cracks under impact or bonds poorly.
The 2024 MarketsandMarkets thermal spray coatings report estimates industry growth from approximately USD 11.7 billion in 2023 to USD 16.2 billion by 2028. This expansion reflects demand from energy, mining, aerospace, and repair operations. Nickel remains commercially important, but material costs can shift. The U.S. Geological Survey’s 2024 Mineral Commodity Summaries reported global nickel mine production near 3.6 million metric tons in 2023. Buyers should therefore compare powder yield, not only purchase price.
For global procurement, request chemistry certificates, particle-size distribution, flowability data, and hardness results tested under ASTM E18 or an equivalent method. ISO 14919 also provides useful requirements for thermal-spray powder supply and classification. In field work, I would inspect the substrate first, especially sharp edges and oil contamination. Small preparation errors become large coating failures. I have seen technically strong powders perform poorly after rushed blasting. That mistake is easy to repeat. Process trials should record spray distance, gas settings, substrate temperature, and coating thickness before volume orders.
Nickel-based self-fluxing powders are widely selected when both wear resistance and corrosion protection are required. The chart shows representative deposited-hardness ranges for common nickel alloy powder families. Actual results vary with alloy chemistry, substrate preparation, heat input, coating thickness, and post-fusion conditions.
2026 Top Spray Welding Powder Types for Global Buyers
Cobalt-based spray welding powders suit high-temperature components exposed to wear, friction, and corrosive gases. Their deposited hardness commonly ranges from 35 to 55 HRC, depending on alloy chemistry and welding conditions. This range supports valve seats, shafts, sealing surfaces, and furnace hardware. At elevated temperatures, cobalt alloys can retain useful hardness better than many iron-based alternatives. However, hardness values should never be treated as guaranteed. Substrate composition, powder size, flame energy, and cooling rate can change the final result.
A sound selection begins with the service environment. Check operating temperature, contact pressure, impact, and chemical exposure. A 55 HRC layer may resist abrasion well, but it can crack under repeated impact. A 35 HRC deposit may offer better toughness. Think beyond the highest number. Surface preparation also matters. Degreasing, controlled preheating, and careful dilution improve bonding. In field work, poor preparation often causes more failures than powder choice.
Tips: Request a lot-specific chemical analysis and particle-size report. Confirm hardness using the same test method and load. Apply a test coupon when the component is costly or difficult to replace. Inspect for pores, cracks, and uneven fusion after machining. Keep records of torch distance, travel speed, and cooling time. Small process changes matter. Even experienced teams sometimes overlook them.
| Cobalt-Based Powder Type | Typical Nominal Chemistry (wt%, balance cobalt) |
Typical Hardness | Approx. Solidus–Liquidus Range | Common Powder Size for Spray Welding | Recommended Deposition Method | Typical Application Areas | Key Performance Characteristics |
|---|---|---|---|---|---|---|---|
| Cobalt–Chromium–Tungsten–Carbon, High-Carbon Grade | Cr 25–30%; W 8–12%; C 1.0–1.5%; minor Si and Mn | 48–55 HRC | Approximately 1,250–1,350 °C | 45–106 µm | Oxy-fuel spray welding with controlled fusion; suitable for localized repair | Valve seats, hot shears, cutting edges, pump wear parts, and furnace hardware | High resistance to abrasive wear, metal-to-metal wear, oxidation, and elevated-temperature softening; carbide-rich structure can reduce impact toughness |
| Cobalt–Chromium–Tungsten–Carbon, Medium-Carbon Grade | Cr 25–30%; W 4–8%; C 0.7–1.2%; minor Si and Mn | 40–48 HRC | Approximately 1,250–1,350 °C | 45–106 µm | Oxy-fuel spray welding, laser-assisted deposition, or plasma-based deposition | Valve components, hot forming dies, pump sleeves, shafts, and wear-resistant machine parts | Balanced wear resistance and toughness with good hot-hardness retention; generally more damage-tolerant than high-carbon grades |
| Cobalt–Chromium–Tungsten–Carbon, Low-Carbon Grade | Cr 25–30%; W 3–6%; C 0.2–0.5%; minor Ni, Si, and Mn | 35–42 HRC | Approximately 1,250–1,360 °C | 45–90 µm | Oxy-fuel spray welding or laser cladding when lower dilution is required | Thermal-processing fixtures, valve bodies, sliding surfaces, and components exposed to thermal cycling | Improved toughness and crack resistance, good corrosion resistance, and reliable performance under repeated heating and cooling |
| Cobalt–Chromium–Molybdenum–Carbon Grade | Cr 25–30%; Mo 4–8%; C 0.3–0.8%; minor Si and Mn | 35–45 HRC | Approximately 1,230–1,350 °C | 45–106 µm | Oxy-fuel spray welding, plasma transferred arc, or laser cladding | Corrosive wear parts, chemical-processing valves, pump components, and hot fluid-handling equipment | Good resistance to corrosion-assisted wear and cavitation; molybdenum improves resistance to localized corrosion in suitable environments |
| Cobalt–Chromium–Nickel–Tungsten–Carbon Grade | Cr 20–28%; Ni 5–15%; W 5–10%; C 0.8–1.2%; minor Si and Mn | 40–50 HRC | Approximately 1,220–1,340 °C | 45–106 µm | Oxy-fuel spray welding or plasma-based deposition with controlled preheating | Hot working tools, high-temperature shafts, valve trim, and components subject to thermal shock | Good combination of thermal-fatigue resistance, toughness, oxidation resistance, and elevated-temperature wear performance |
| Self-Fluxing Cobalt–Chromium–Nickel–Boron–Silicon Grade | Cr 15–25%; Ni 5–15%; Si 2–6%; B 1–3%; C 0.6–1.2%; balance cobalt | 35–45 HRC | Approximately 1,050–1,180 °C | 45–90 µm | Spray-and-fuse oxy-fuel processing; boron and silicon assist wetting and oxide removal | Low-to-medium temperature shafts, sleeves, guide surfaces, pump parts, and dimensional restoration work | Good bondability and machinability after fusion; suitable for restoration layers, but generally less suited to the highest-temperature service than tungsten-containing grades |
Iron-based spray welding powders remain practical for economical industrial repairs. They rebuild worn shafts, rollers, gear seats, and hydraulic surfaces without replacing entire components. The 45–60 HRC range offers a useful balance between hardness and machinability. However, hardness alone does not guarantee service life. Powder chemistry, dilution, preheating, and finishing control the final result.
The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023. That scale indicates continuing demand for repairable steel equipment.
MarketsandMarkets estimated the thermal spray coatings market at approximately USD 11.9 billion in 2023, with strong growth projected through 2028. Spray welding is only one segment, so this figure should not be treated as direct powder demand.
ASM Handbook guidance also stresses substrate preparation, thermal control, and post-treatment. These details are often underestimated.
Tips: Confirm hardness after deposition, not only from the powder certificate. Use ASTM G65 testing when abrasive wear matters. Keep the repair layer slightly oversized for controlled machining. Preheat thick steel gradually, and monitor interpass temperature. A 60 HRC deposit may resist abrasion well, but it can crack under impact. I have seen specifications chase maximum hardness and overlook toughness. That is a costly assumption. Experienced buyers should request chemistry, particle-size distribution, deposition efficiency, and batch traceability. Local welding procedures still need validation on the actual component.
WC-reinforced powders containing 50–70 vol% tungsten carbide suit components facing severe abrasive wear. Mining chutes, pump sleeves, and drilling tools often benefit from this structure. The carbide particles carry the wear load, while the metallic binder supports adhesion and impact resistance. In practical coating work, carbide size matters as much as volume percentage. Fine particles can produce smoother layers. Coarser particles may resist cutting wear more effectively.
A higher carbide fraction sounds better, but it is not always better. Excess carbide can reduce toughness and increase cracking risk during heating or service. Binder chemistry, substrate preparation, spray temperature, and coating thickness must match the application. Experienced technicians inspect cross-sections, hardness, porosity, and bond quality before approving production.
A hard surface alone proves little. I have seen excellent laboratory hardness fail under repeated impact. That lesson is easy to overlook.
Tips:
Confirm the wear mechanism before selecting powder. Check whether the part faces cutting abrasion, sliding wear, or impact. Request particle-size data and carbide volume information from suppliers. Test a small coated section first. Keep process records, including surface roughness and preheating temperature. One detail can change results. Also review machining needs, because 70 vol% carbide coatings may demand diamond tooling and slower finishing.